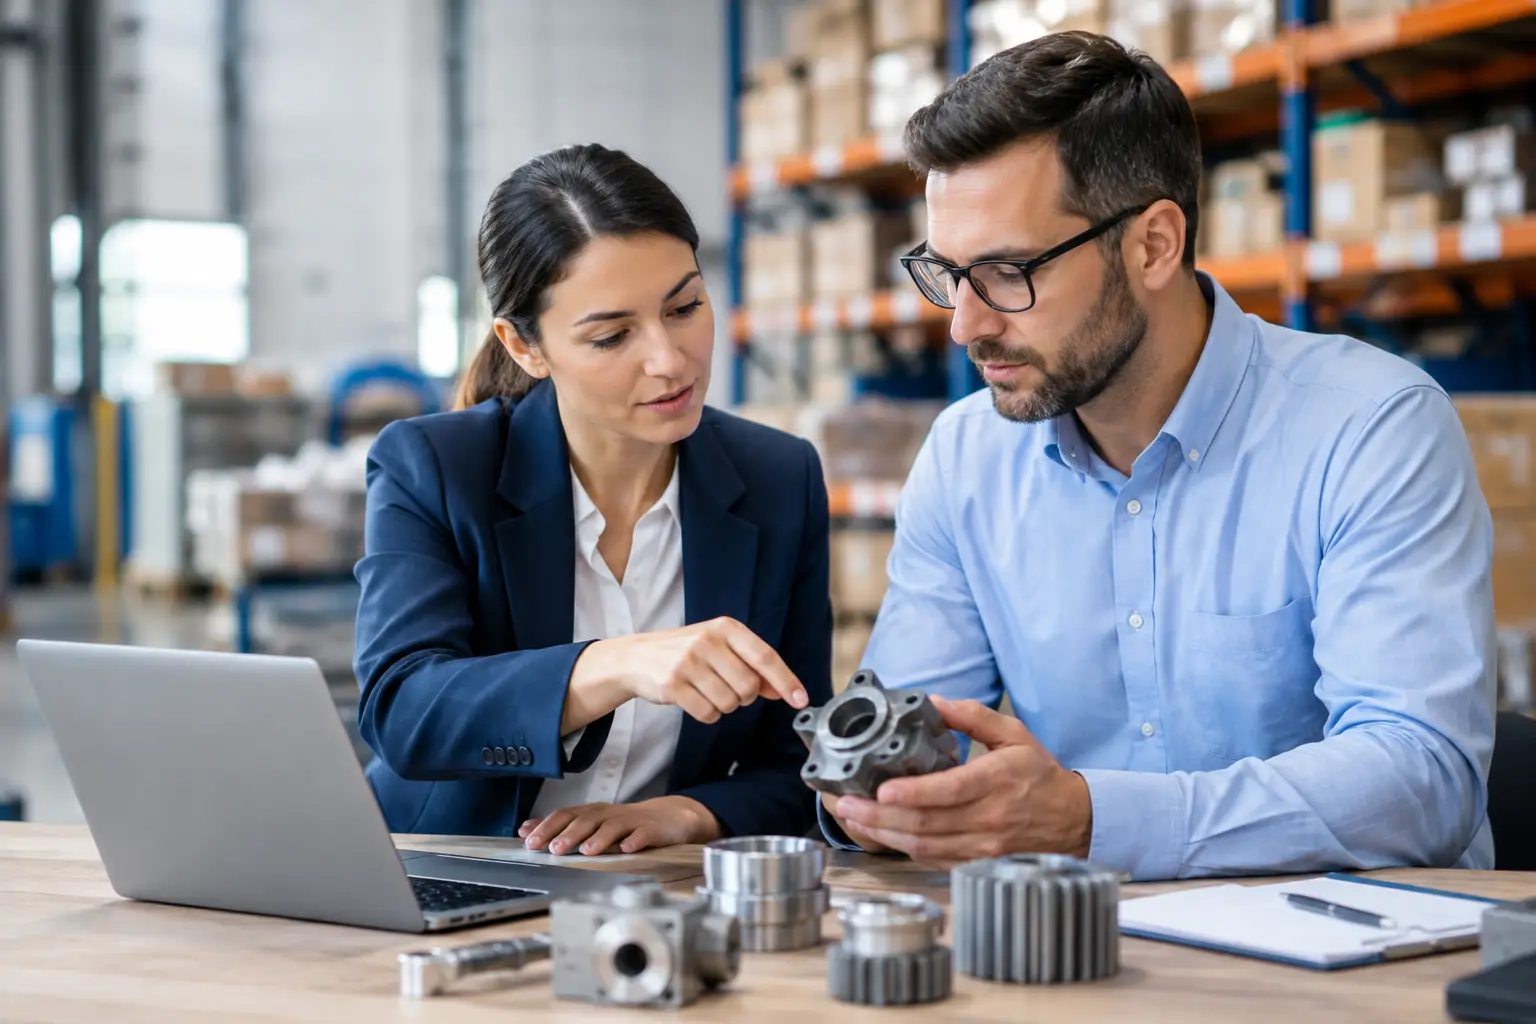
A drawing can look complete and still leave the most expensive questions unanswered. Can the radius be formed consistently? Will the coating affect a critical fit? Is the specified material available at production volumes? For teams developing precision parts, industrial component supplier management is where these questions are resolved before they become late-stage quality issues, delayed launches or costly tooling changes.
This is not simply a purchasing discipline. When a component has tight tolerances, specialised materials or an unfamiliar production route, supplier management is a technical process. It connects design intent with manufacturing reality, while protecting quality, delivery and long-term continuity of supply.
What effective supplier management really involves
A supplier can meet a quoted unit price and still be the wrong manufacturing partner. The best choice depends on more than capability statements or a sample part. It depends on whether the manufacturer understands the functional requirement, can control the relevant process variables and has the capacity to support the product beyond its first production run.
For a deep-drawn metal component, that may mean assessing wall-thickness variation, draw ratios, tooling life and secondary operations. For a micro spring or wire form, the conversation may centre on force curves, fatigue life, material condition and repeatability. With micro silicone parts, cleanliness, moulding behaviour and post-processing may be just as significant as the nominal dimensions.
Effective management therefore brings engineering, quality, procurement and operations into the same conversation early enough to make a difference. It replaces the unhelpful question, “Who can make this?” with a more useful one: “Who can make this reliably, at the required performance level and within the actual commercial constraints?”
Start with the function, not only the drawing
The drawing remains essential, but it is not always the full specification. Dimensions indicate what must be produced; they do not necessarily explain what matters most in use. A feature may require a tight tolerance because it interfaces with a sealing surface, controls an optical path or determines sensor alignment. Another apparently tight feature may have more latitude than the drawing suggests.
That distinction has a direct effect on manufacturability and cost. If every dimension is treated as critical, the supplier may need slower processes, additional inspection or unnecessarily complex tooling. If a genuinely functional feature is under-specified, variation can appear only when the finished assembly is tested.
A productive technical review should establish the component’s job, interfaces, material requirements, operating environment and failure modes. It should also clarify annual demand, batch sizes, expected product life and any ramp-up profile. A part required in annual volumes of 5,000 has different economic and process implications from the same part needed at 500,000 units.
This is where a local, technically fluent contact adds real value. Rather than passing a drawing through several layers of communication, the team can translate requirements into the language of the relevant process and bring practical feedback back to design and purchasing.
Treat tolerances as a system
Tolerances do not exist in isolation. A component can be within its individual dimensional limits yet still fail in an assembly because of stack-up, surface condition, concentricity or material behaviour. This is particularly relevant for miniature components, sensor housings, optical assemblies and medical technology applications, where small deviations can have large functional consequences.
The right supplier-management process identifies critical-to-function characteristics and agrees how they will be measured. That may involve gauge strategy, sampling plans, capability targets, first article inspection and process validation. The aim is not to inspect quality into every batch. It is to build a process capable of producing the required result repeatedly.
Match the supplier to the manufacturing process
A broad supplier base can appear safer, but it often creates more administration without improving resilience. The better approach is to build access to specialist manufacturers whose process expertise fits the component challenge.
For example, a precision metal-cut part may call for different knowledge from a deep-drawn cup, even if both are made from similar alloys. Ultrasonic machining can be a strong option for hard and brittle materials where conventional machining risks damage or excessive tool wear. Powder compaction requires an understanding of powder flow, density distribution and the trade-offs between isostatic and mechanical compaction. For PIR lens solutions and LED modules, optical performance, material selection, thermal behaviour and production consistency need to be considered together.
Supplier selection should test four connected areas:
- Technical fit: Does the manufacturer have proven experience with the material, geometry and process window required?
- Quality control: Can it demonstrate meaningful inspection methods, traceability and corrective-action discipline?
- Operational fit: Are capacity, lead times, logistics and communication compatible with the programme?
- Commercial continuity: Is the supplier positioned to support tooling maintenance, engineering changes and future demand?
None of these categories should automatically outweigh the others. For a safety-critical aerospace part, process control and traceability may be decisive. For an early-stage development programme, engineering responsiveness and willingness to iterate might matter more. For a mature high-volume product, capacity planning and cost stability can become the leading concerns.
Industrial component supplier management during development
The most valuable supplier involvement often happens before a purchase order is placed. Early manufacturing input can reveal a more stable geometry, a better material thickness or an alternative process that simplifies production without compromising function.
It is sensible to involve the manufacturing partner when designs are still adaptable. Waiting until drawings are released may feel orderly, but it can lock in assumptions that are difficult to reverse. A tooling change after validation is rarely a minor event, especially when the component has interacting features or requires specialised forming, moulding or coating processes.
A disciplined development path normally moves from feasibility assessment to samples or prototypes, then to tooling approval, first articles, validation and controlled serial production. The exact sequence varies. A simple wire form may progress quickly, while a multi-operation deep-drawn component or a tightly specified optical solution may need several review cycles.
At each stage, document decisions clearly. Record agreed materials, approved samples, inspection expectations, packaging requirements and deviations. Informal knowledge is useful, but it should not be the only place critical information lives. Clear documentation protects both parties when teams change, volumes rise or a product returns for redesign years later.
Build communication into the supply model
Many supplier problems are communication problems that arrive disguised as quality or delivery problems. A revised drawing is issued but not acknowledged. A forecast changes without context. A supplier flags a tooling risk, but the message reaches purchasing rather than the design engineer who can act on it.
A strong operating rhythm prevents these gaps. For active projects, regular technical and commercial reviews keep progress visible. These discussions should cover open design points, qualification status, tooling milestones, capacity, material availability and delivery risks. When a problem is identified, the focus should be on containment first, root cause second and prevention third.
There is a balance to strike. Excessive meetings slow decisions and burden specialists. Too little contact allows assumptions to multiply. The right frequency depends on project maturity and risk. Development programmes require close collaboration; stable production may need only planned performance reviews, alongside a clear escalation route when circumstances change.
Use data without losing engineering judgement
Supplier scorecards are helpful when they lead to useful action. On-time delivery, non-conformance rates, response times and corrective-action closure can show trends that individual incidents hide. Yet numbers alone can mislead. A low defect rate may reflect very low volumes. Excellent delivery performance may be supported by large buffers rather than a predictable process.
Combine performance data with technical insight. Ask whether recurring issues concentrate around a particular operation, material batch or product family. Look at the cost of poor quality, not merely the number of rejected pieces. A small defect in a micro component can stop an entire high-value assembly line.
The same principle applies to cost reduction. A lower piece price can be attractive, but it may be offset by higher incoming inspection, longer lead times, greater inventory or weaker support when changes are needed. Total cost includes the time spent managing exceptions.
Make resilience practical, not theoretical
Recent supply disruptions have made dual sourcing a familiar topic. It can be sensible, but it is not always straightforward. Replicating a specialised manufacturing process at a second supplier may require fresh tooling, validation and substantial engineering effort. For highly customised components, two nominally equivalent suppliers may still produce parts with meaningful process differences.
Resilience can also come from practical measures: realistic forecasts, agreed safety-stock policies, visibility of long-lead materials, tooling maintenance plans and early warning when demand shifts. In some cases, a single specialist supplier with transparent communication and carefully managed inventory is less risky than two poorly aligned sources.
JVS Sales & Technical Consultants helps customers coordinate these decisions across a network of specialist manufacturers, giving project teams a local technical contact while retaining access to process-specific expertise.
The relationship is part of the component
Precision components do not become dependable because a supplier has been approved once. They become dependable through continued technical dialogue, process discipline and a shared understanding of what the finished product must do. The supplier relationship is therefore part of the component’s performance, even though it never appears on the drawing.
When the next design review raises a question about a tiny radius, a coating thickness or an unexpectedly difficult material, bring the manufacturing conversation forward. Small parts can carry big consequences, and the best time to manage them is while there is still room to improve the design.