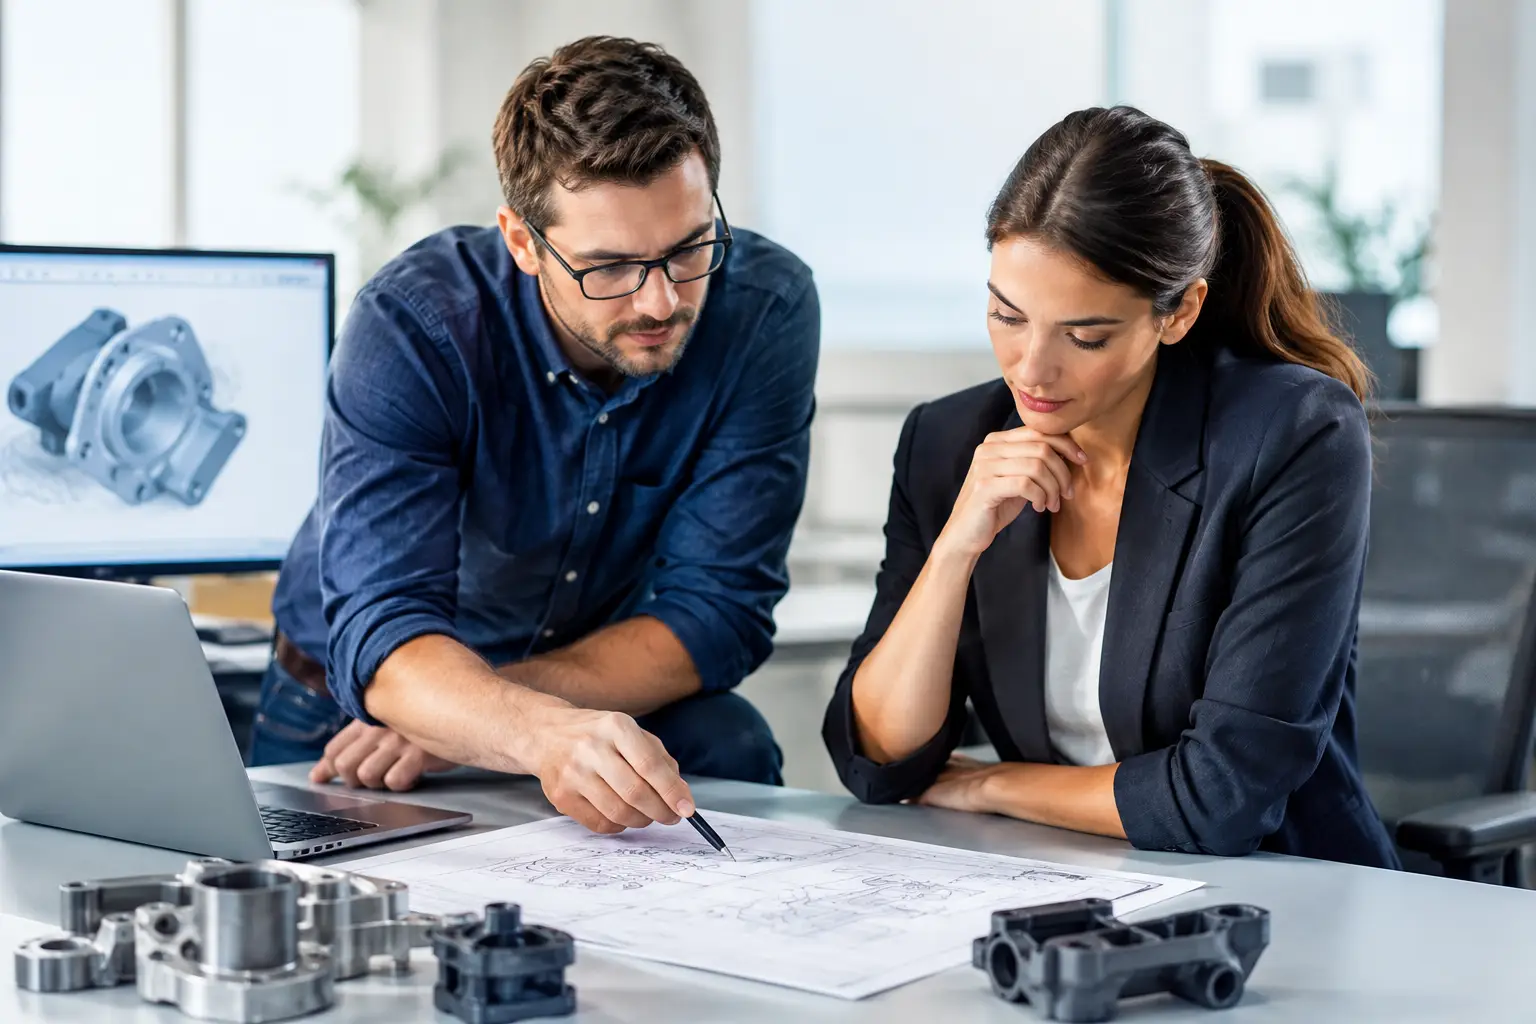
A drawing can look perfectly sensible until a production engineer asks the questions that decide whether it can be made consistently: How will the material behave? Where is the datum? Can the feature be measured? What happens when tooling, tolerances and volume requirements meet? Design for manufacturability engineering support brings those questions forward, while changes are still measured in hours rather than expensive tooling rework.
For precision small parts, this early work is rarely optional. A deep-drawn cup, micro spring, wire form, cut metal part or silicone component may be only millimetres in size, yet its geometry can place demanding limits on tooling, material flow, inspection and assembly. The objective is not to dilute an ambitious design. It is to preserve the function that matters while creating a dependable route to production.
Why manufacturability must be considered early
The most costly design decisions are often made before a supplier has seen the component. A nominal wall thickness may be technically possible but unsuitable for deep drawing at the specified depth. A sharp internal corner may complicate a machined feature. A tolerance applied across every dimension may drive inspection effort and scrap without improving product performance.
Manufacturability support makes these dependencies visible. It connects the design requirement to a realistic process window, including material grade, forming direction, tool access, springback, burr control, coating thickness and measurement capability. That connection is particularly valuable where several manufacturing processes could produce the part, but with very different cost, lead-time and quality profiles.
There is no single rule that says a feature is manufacturable or not. The answer depends on annual volume, material, critical dimensions, downstream assembly and acceptable risk. A machining route can be sensible for prototypes and low quantities, while a formed or stamped solution may be the better long-term choice. Good engineering support does not force every project towards the same process. It tests the assumptions behind the specification and selects a route that fits the application.
What design for manufacturability engineering support should deliver
Useful support is more than a design review with a red pen. It should give product teams clear options, explain the consequences of each option and help them make decisions early enough to protect the programme.
The work usually begins by identifying the part’s true functional requirements. Which dimensions locate the component? Which surfaces seal, carry load, conduct electricity or guide a sensor? Which cosmetic requirements are customer-facing, and which are simply inherited from an early CAD model? Separating critical features from non-critical ones is often the fastest route to a more producible component.
From there, the engineering discussion should cover process suitability. For a deep-drawn component, that may mean draw ratios, radii, material grain direction and whether secondary operations are needed. For micro springs and wire forms, it can involve wire diameter, coil index, stress levels, end configuration and automated handling. For precision cut parts, it may focus on burr direction, strip layout, tooling wear and the relationship between tolerances and the chosen material thickness.
A practical output includes a manufacturability assessment, proposed geometry changes where necessary, material recommendations, tolerance guidance and a clear view of prototype versus serial-production methods. When the part interfaces with other components, assembly and inspection should be considered at the same time. A part that is easy to make but difficult to orient, measure or fit is not yet a production-ready solution.
Tolerances need a purpose
Tight tolerances are sometimes essential. In medical technology, sensor assemblies, aerospace components and semiconductor equipment, a few microns can determine fit, signal quality or safety. But the tightest tolerance on every feature is not a sign of engineering maturity. It can limit the available manufacturing routes, increase tool maintenance and turn otherwise capable suppliers away from the project.
The better question is: what variation can the final product tolerate? Functional tolerancing, supported by appropriate datums and measurement strategy, concentrates control where it delivers value. It also gives the manufacturer a fair basis for process capability planning. In many cases, changing a non-functional tolerance, adjusting a radius or specifying a realistic surface condition has no negative effect on performance and a meaningful effect on yield.
Materials and finishes are part of the design
Material selection should not be treated as a line item added at the end of the drawing. A stainless steel grade, copper alloy, nickel material or technical silicone can affect forming behaviour, fatigue life, conductivity, corrosion resistance and supply continuity. The same is true of coatings and surface treatments, which can change dimensions, friction, solderability and visual appearance.
This matters when a component serves several functions. A small metal part may need to be springy, corrosion-resistant and suitable for a coating process. A silicone element may need to withstand a cleaning agent while maintaining dimensional stability. The right material is therefore the one that works across the full manufacturing and operating environment, not merely the one that meets a headline property on a data sheet.
From CAD model to a stable production process
A strong review moves in stages. Early sketches and CAD data establish the functional intent. A supplier-level feasibility assessment then tests the geometry against real equipment, tools and process knowledge. Prototype parts provide physical evidence, but they must be interpreted carefully: a hand-finished prototype may prove a concept without proving that the same quality can be repeated at production rate.
Before serial production, teams should agree the control plan. This includes the features to inspect, measurement methods, sampling logic, packaging and traceability requirements. For miniature parts, handling deserves particular attention. A component can meet its drawing tolerance and still become unusable if it tangles, is scratched in transit or cannot be reliably fed into an automated assembly system.
The transition between stages is where project coordination earns its place. Design engineering may be focused on performance, purchasing on commercial continuity and operations on cycle time and delivery reliability. Each view is valid, but they need to meet around the same specification. A local technical contact who can coordinate specialist manufacturers reduces the risk of important details being lost between CAD release, quotation, tool build and first article approval.
At JVS Sales & Technical Consultants, this is the practical value of a specialist partner network: access to process-specific knowledge without asking the customer to manage a different niche supplier for every technical question. The discussion can begin with the application and move towards the right manufacturing route, whether the answer lies in deep drawing, micro springs, precision cutting, silicone moulding, advanced machining or a related process.
Common issues that deserve an early conversation
Some design problems recur because they are easy to miss on screen. Avoiding them does not require a lengthy workshop, but it does require the right people to look at the part before tooling is committed.
- Specifying internal corners or slots that a chosen tool cannot reach without a secondary operation.
- Calling out general tolerances that conflict with the functional datum scheme.
- Designing features that require manual orientation during assembly.
- Assuming a prototype process will scale directly to the required annual volume.
- Selecting a finish without accounting for its dimensional build-up or masking requirements.
These are not reasons to simplify every component. They are prompts for a useful engineering conversation. Sometimes the specified feature is non-negotiable, and the correct response is to select a more capable process or accept a higher unit cost. What matters is that the trade-off is deliberate, visible and agreed before it becomes a production problem.
Better collaboration creates better components
The most effective manufacturability work is collaborative rather than transactional. Share the operating environment, forecast volumes, assembly method and failure modes alongside the drawing. Invite manufacturing input when the geometry still has room to change. Ask for alternatives, not just a yes-or-no feasibility response.
This approach is especially valuable for products that combine precision mechanics with sensing or lighting. A PIR lens, LED module, metal housing and retention feature can each be individually well designed while still creating tolerance-stack or assembly challenges as a system. Reviewing interfaces early helps preserve optical performance, reliable detection and repeatable final assembly.
A production-ready design is not the one with the fewest features. It is the one whose critical features can be made, measured and supplied repeatedly at the quality level the application demands. Bring the manufacturing conversation to the first serious drawing review, and the project is far more likely to reach production with fewer surprises and better choices still available.